
Hangbo Alloy Group
Shanghai · Est. 2012
What does a hardness test actually tell me about a nickel alloy?
It tells you the metallurgical condition of the lot: a soft, solution-annealed reading, a hard, age-hardened band, or an elevated, cold-worked value. Hardness tracks dislocation density, precipitates and grain structure, so it is the fastest field evidence that the alloy was delivered in the state you ordered, independent of chemistry. It does not by itself prove composition, which is why it is paired with chemical analysis and positive material identification on a critical order.
A hardness number can look right and still hide the wrong condition. This guide shows the eight ways a nickel alloy hardness report misleads a buyer, the scales & conversions that matter, the ASTM standards that govern the test, and the purchase-order clauses that keep a false-soft result out of your equipment.
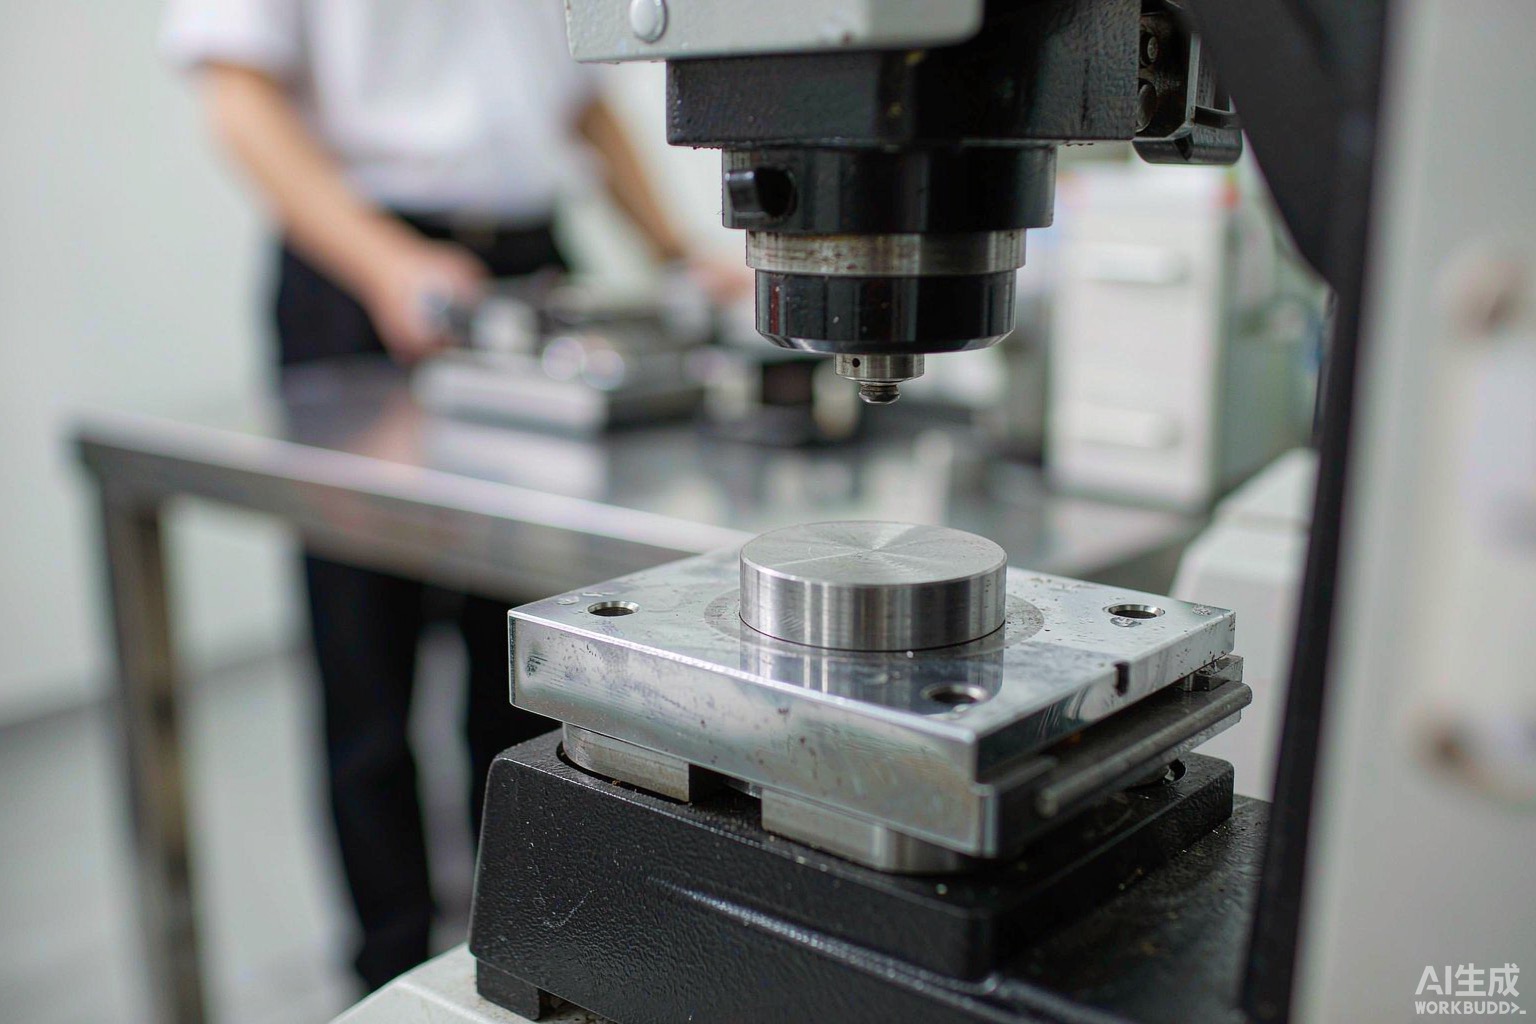
Short answer: a hardness test presses a known indenter into the metal under a known load and measures the impression, and verifying the report means confirming the scale, load, location, number of readings and acceptance window were correct for your alloy and condition — not just trusting a single number. This guide covers what a genuine hardness report must list, the eight ways a hardness figure misleads a buyer, how Rockwell, Brinell and Vickers scales differ and convert, how to use hardness as a heat-treatment acceptance gate, and the purchase-order clauses that keep a false-soft result out of your equipment.
Nickel alloys are bought for a metallurgical state, not just a chemistry. The same UNS number can arrive solution-annealed and soft, age-hardened and strong, or cold-drawn and work-hardened, and hardness is the fastest field check that tells those states apart. A tensile coupon takes a machined sample and a lab; a hardness reading takes a few seconds on the part itself. That speed is exactly why hardness is the control a buyer should demand on every critical lot — and exactly why a tampered hardness line is the cheapest way to ship the wrong condition.
We are a Shanghai maker of nickel-based and high-temperature alloys, and our line runs from a fully virgin prime charge into VIM plus ESR or VAR, through careful descaling, conventional forge and roll, the ordered solution or precipitation heat, and a full in-house check: spectrometry with wet chemistry, mechanical and NDT coverage, and dimensional verification — so the hardness we record is measured on the exact heat we shipped, not a number borrowed from elsewhere. The reason for detailing that chain is simple: the figure on the certificate should be reproducible from the very bar you received, and this guide helps you confirm that it is.
Short answer: hardness tracks the internal structure of the metal — dislocation density from cold work, precipitates from aging, grain structure from heat treatment — so a single reading tells you within seconds whether the alloy is in the soft, solution-treated state or the hard, aged state you specified, well before a tensile result returns from the lab.
The mechanism is physical. A metal resists indentation because of the obstacles inside its crystal lattice: grain boundaries, dissolved atoms, fine precipitates and tangled dislocations. Cold working multiplies dislocations and drives hardness up. A full solution anneal dissolves those strengthening phases and drops hardness to its lowest point. Age hardening or precipitation strengthening then grows nanometer-scale particles that lock dislocations and push hardness back up into a defined band. For an age-hardenable grade the production control is, in practice, a hardness window: too low means under-aged or wrongly annealed, too high can mean over-aged or a different thermal path.
That is also why hardness is the first place a shortcut shows up: shipping solution-annealed stock where age-hardened was ordered is invisible to a chemistry or dimension check but glaring on a hardness tester, and a cold-drawn bar sold as annealed will read hard. The test is cheap and hard to argue with — which is exactly why a dishonest supplier manipulates the report, not the metal. For welds, hardness at the heat-affected zone predicts cracking resistance, and our welding nickel alloys guide explains why the procedure, not the filler, keeps that zone sound.
Short answer: a defensible hardness report names the scale and indenter, the applied load, the test location on the part or coupon, the number of readings and their spread, the recorded mean, any conversion performed, and the heat or lot the readings tie to — and it states the acceptance window the values were judged against.
A bare “HRC 35” with no context is not a measurement you can act on; it is a number detached from the part. The table below lists what a credible report must state and the red flag when a field is missing or vague.
| Field on the report | What it should state | Red flag if absent or vague |
|---|---|---|
| Scale & indenter | Rockwell C (HRC), Rockwell B (HRB), Brinell (HBW), or Vickers (HV) with ball/diamond spec | Only “hardness” with no scale named |
| Applied load | The major load in kgf / N (e.g. HRC 150 kgf, HBW 10/3000) | Load omitted so conversion cannot be checked |
| Test location | Surface vs core, specific face, distance from end | Single number with no position recorded |
| Readings & spread | Count of impressions and the minimum–maximum range | One value presented as the whole story |
| Mean & acceptance | Calculated average against the stated window | Mean given but no acceptance band cited |
| Conversions | Any scale conversion named with the table used | Silent conversion between incompatible scales |
| Heat / lot tie | Heat number and part identification | Result not linked to your specific lot |
| Surface condition | Preparation (ground, polished) and decarburization check | Test taken through scale or a soft skin |
Note the spread and the location. A report that lists a single reading tells you almost nothing, because hardness varies across a forging or a bar — a soft centre, a hard surface or a cold-worked rim all hide behind one number. A genuine report maps several impressions and shows the range, so you can judge whether the lot is uniform or carrying a soft spot.
Short answer: a hardness result misleads when the wrong scale was used for the alloy, the section was too thin for the load, a cylindrical surface was not corrected, one reading stood in for many, the heat treatment was not actually performed, a scale was converted incorrectly, the surface was tested through scale or a decarburized skin, or no test was done at all — and each mode has a specific detection step.
| Problem | Root cause | Symptom you see | How to detect | How to prevent |
|---|---|---|---|---|
| Wrong scale for condition | HRC used on soft annealed stock or on a thin section | Shallow, meaningless indent; number looks plausible | Confirm scale matches the alloy hardness range | Name scale and load in the PO |
| Thin-section anvil effect | Load too high for the thickness | Reading reads low (anvil supports the indent) | Check thickness vs load table in ASTM E18 | Specify minimum thickness per load |
| Uncorrected curve | Cylindrical part tested without correction | Apparent hardness off by several points | Apply the diameter correction in the standard | Require correction factor on rounds |
| One reading only | Single impression presented as representative | Clean number hides a soft or hard spot | Demand a map of ≥3–5 impressions with range | Clause for count and location |
| Heat treat not done | Material shipped in the wrong condition | Number outside the ordered window | Compare to the condition-specific band | Name required condition & window |
| Bad conversion | HRC silently “converted” to HBW across families | Converted value wrong for the alloy | Verify conversion table and material class | Forbid silent conversions in PO |
| Surface skin | Test taken through oxide scale or decarb layer | Reading reads low on the outside | Insist on prepared, scale-free surface | State surface prep in the spec |
| No test performed | Figure written without measuring | No raw data, no map, no lab ID | Request raw readings and lab accreditation | Third-party witness or retention |
The two most damaging failure modes are the wrong-scale reading and the silent conversion. A plausible number on the wrong scale looks authoritative and is still meaningless, and a Brinell value converted from Rockwell across a different alloy family can miss the tolerance you are holding by far more than the band allows. Both are exposed the moment you read the scale, the load and the conversion rule. Where long-term strength matters more than surface hardness, the same lot should also be judged on high-temperature behaviour — our creep and stress-rupture guide explains why a hard number today is no promise of life under load.
Short answer: Rockwell measures depth recovery under load, Brinell measures the diameter of a ball impression, and Vickers measures the diagonal of a diamond pyramid impression — they are not interchangeable, and any conversion between them is approximate and valid only within the same material class and hardness range.
Each scale suits a different regime. Rockwell is fast but its shallow indent makes it sensitive to surface condition and thin sections. Brinell spreads the load over a wide ball impression, averaging a larger volume, which suits coarse or uneven material such as castings and large forgings. Vickers uses a pyramid so one indenter covers the full range and underpins microhardness on a polished mount — the way you read a carburized or nitrided case depth.
| Scale | Indenter | Typical load | Best for | Conversion caveat |
|---|---|---|---|---|
| Rockwell C (HRC) | 120° diamond cone | 150 kgf | Hardened, heat-treated stock | Invalid below ~HRC 20; use HRB there |
| Rockwell B (HRB) | 1.588 mm ball | 100 kgf | Soft annealed and cold-drawn stock | Use where HRC would be too shallow |
| Brinell (HBW) | Tungsten-carbide ball | Usually 10/3000 or 2.5/187.5 | Castings, forgings, coarse grain | Averages a larger area than Rockwell |
| Vickers (HV) | 136° diamond pyramid | 1–120 kgf (micro to macro) | Case depth, thin layers, full range | Most consistent across ranges |
The conversion caveat is the part buyers ignore. Conversion tables (ASTM E140, ISO 18265) are empirical and built for specific material families; applying a steel conversion to a nickel superalloy can be badly wrong because indentation recovery differs between alloys. If a report gives HRC but your specification speaks in HBW, insist the conversion uses the correct table and shows both original and converted values — never accept a converted number with no trace of the scale actually measured.
Short answer: every ordered condition carries a documented hardness window in the material standard or the purchase order, and acceptance means confirming the measured value lands inside that window for the correct condition — soft for solution-annealed, within band for age-hardened, elevated for cold-worked — rather than accepting a bare figure.
The direction is easy to reason about. A fully solution-annealed nickel alloy is at its softest because the strengthening phases are dissolved; an age-hardened variant of the same alloy is markedly harder because fine precipitates have formed; a cold-drawn bar is harder still at the surface than its annealed cousin. So an age-hardened order reading in the soft, solution-treated range flags a skipped aging step or a wrong condition shipped, and an annealed order reading hard means the material was work-hardened or never softened. The window itself comes from the grade specification, and verifying means checking the measured value against that named window and confirming the window matches the condition you ordered. Over-aging is the opposite failure — holding too long or too hot coarsens the precipitates and can soften the part while inviting brittle intermetallics, a mechanism our sigma-phase guide covers.
| Ordered condition | Expected hardness direction | What a wrong reading signals |
|---|---|---|
| Solution annealed | Lowest for the grade | Hard reading → cold work or no anneal |
| Age / precipitation hardened | In a defined mid-to-high band | Soft reading → under-aged or skipped aging |
| Cold worked / drawn | Elevated vs annealed | Soft reading → not work-hardened as claimed |
| Over-aged | Dropping below the aged band | Soft + brittle → excessive thermal exposure |
For age-hardenable grades the line lives or dies on this gate, which is why our own age-hardening route is controlled by hardness at multiple points and why the precipitation-strengthening guide describes what the hardening particles do inside the metal. A buyer who asks for the hardness window on the order, and receives the readings with their spread, turns a vague “heat treated” claim into a measurable, enforceable requirement.
Short answer: the test method is fixed by ASTM E18 (Rockwell), E10 (Brinell) and E92/E384 (Vickers, including microhardness), conversions by ASTM E140, the international equivalents by ISO 6506 / 6507 / 6508, and the lab credibility by ISO/IEC 17025 — verification is confirming all of these are named and consistent on the report.
The method standard and the acceptance window are different documents, and confusing them is a classic buyer error. ASTM E18 tells you how to apply the Rockwell indenter and read the depth; it does not set the hardness your age-hardened part must reach — that target comes from the material specification or the purchase order. Always confirm the report cites the method standard with its edition year and that the acceptance band matches the one on your order. In sour or corrosive duty the hardness ceiling can be tied to cracking resistance, and our sour gas selection guide explains why an upper limit can matter as much as a lower one.
| Document | Role | What to verify |
|---|---|---|
| ASTM E18 | Rockwell hardness method | Scale, load, indenter, correction |
| ASTM E10 | Brinell hardness method | Ball diameter, load, dwell |
| ASTM E92 / E384 | Vickers / microhardness method | Pyramid load, optical measurement |
| ASTM E140 / ISO 18265 | Hardness conversions | Convert only within the right family |
| ISO 6506 / 6507 / 6508 | International hardness methods | Edition matches the PO |
| ISO/IEC 17025 | Lab competence | The testing lab is accredited |
Where a grade swap could hide inside the lot, hardness alone will not prove chemistry, and our nickel vs stainless selection guide shows why the two families can read alike on some scales yet behave nothing alike in service. Hardness is a condition check, not an identity check — pair it with positive material identification when the alloy itself is in doubt.
General references: Nickel Institute · AMPP · SAE International · ASTM International
Short answer: write the scale and load, the minimum section thickness for that load, the cylindrical correction, the required number and map of readings, the acceptance window from the specification, the surface preparation, the conversion rules, and a data-retention or third-party clause directly into the purchase order — vague “hardness tested” language is the loophole this whole problem hides behind.
A spec that says “material to be hardness tested” has not specified anything enforceable. The clauses below turn a suggestion into an auditable requirement, expected on any serious nickel-alloy order where the condition decides whether the part survives.
| Clause | What it must say | What it stops |
|---|---|---|
| Scale & load | “Hardness per ASTM E18, HRC 150 kgf (or named scale)” | Wrong-scale, meaningless indents |
| Section thickness | “Thickness ≥ minimum per ASTM E18 for the load” | Anvil-effect low readings |
| Curve correction | “Cylindrical correction applied per standard” | Uncorrected round-bar errors |
| Reading count | “≥5 impressions mapped; range reported” | Single-reading cover stories |
| Acceptance window | “Within the band named in the material spec” | Wrong-condition shipments |
| Surface prep | “Ground, scale-free, decarb checked” | False-low surface-skin readings |
| Conversion rule | “Conversions only per ASTM E140, family stated” | Silent, wrong conversions |
| Retention | “Raw readings & lab ID retained, available” | Numbers with no test behind them |
Most failure modes in this guide disappear the moment the purchase order names a scale, a load, a location map and an acceptance window. For the broader substitution and mis-certification risks a buyer faces, the procurement pitfalls guide collects the clauses that close the other loopholes, and for cyclic thermal duty the same discipline protects against cracking a single room-temperature number will never reveal, as our thermal fatigue guide describes.
Short answer: before you accept a hardness report, confirm the scale and load suit the alloy and condition, the section was thick enough for the load, any curve was corrected, several mapped readings with their range were taken, the value falls inside the named acceptance window, the surface was prepared, any conversion is traceable, and the raw data and lab identity are retained — and keep a copy of the readings.
If any single line above cannot be confirmed from the supplied documents, the lot is unverified for condition regardless of how authoritative the headline number looks. Treat a missing scale, load or single reading as a failed check, not a paperwork nuisance — those fields prove the indent was real, correctly placed and fairly measured.
It tells you the metallurgical condition of the lot: a soft, solution-annealed reading, a hard, age-hardened band, or an elevated, cold-worked value. Hardness tracks dislocation density, precipitates and grain structure, so it is the fastest field evidence that the alloy was delivered in the state you ordered, independent of chemistry. It does not by itself prove composition, which is why it is paired with chemical analysis and positive material identification on a critical order.
Because hardness-conversion tables are empirical and tied to a material family and a hardness range; applying a steel conversion to a nickel superalloy can be substantially wrong, since indentation recovery differs between alloys. If you need a converted value, insist it is done with the correct table (ASTM E140 or ISO 18265) for the right family, and that both the originally measured scale and the converted figure are shown so the conversion is traceable.
Compare the reported hardness against the acceptance window named in the material specification for the age-hardened condition. An age-hardenable grade that reads in the soft, solution-treated range has either skipped the aging step or been shipped in the wrong condition. The defence is to name the required condition and its hardness window on the purchase order and to require several mapped readings rather than a single number that could hide a soft spot.
When the test load is too high for the thickness of the piece, the indenter senses the support anvil beneath the sample and the reading comes out artificially low. The method standards set a minimum thickness for each load; avoid it by specifying that thickness rule in the purchase order and by confirming on the report that the section met the minimum, or by using a load and scale matched to a thin section such as Vickers or a lighter Rockwell load.
For a given alloy family and condition there is a broad empirical correlation between hardness and ultimate tensile strength, and conversion charts exist, but it is approximate and breaks down across different alloy families and heat-treatment states. Use hardness as a condition and acceptance check, and rely on the actual tensile test from the mill certificate for design strength — never substitute one for the other on a safety-critical part.
Yes, within limits. Hardness mapping across a weld and its heat-affected zone is a standard way to confirm the joint was not sensitized or over-tempered and to check that the zone is not so hard it risks cracking, which matters in sour or cyclic service. But hardness on a weld is local and directional; it complements rather than replaces volumetric and visual inspection, and the technique and acceptance limits should be named on the welding procedure specification.
Name the scale and load (ASTM E18 Rockwell, etc.), the minimum section thickness for that load, the cylindrical correction, a required count and map of readings with their range, the acceptance window from the material specification, the surface preparation, the conversion rules, and a clause retaining the raw readings and lab identity. Vague “hardness tested” language is the loophole this entire problem hides behind, so the clauses must be specific and auditable.
If your next nickel-alloy order depends on the delivered condition — annealed, age-hardened or cold-worked — tell us the alloy, the form, the governing specification and the service, and we will measure hardness on the exact heat we ship using the scale and load your condition requires, map several impressions across the lot, judge the mean against the named acceptance window, and keep the raw readings on retention — so the number on the certificate is one we can reproduce from the very bar you received, not a figure we hope you never question.
Email: [email protected]
Phone: +86-136-1165-6360
WhatsApp: +86 13611656360
Send us the alloy, the form, the governing specification and the service severity — and we will name the hardness scale and load that fit the condition, map the readings across your lot, confirm the mean against the acceptance window, and supply material whose delivered state is measured and recorded, with the raw data available for your inspector to re-check.