
Hangbo Alloy Group
Shanghai · Est. 2012
The low-carbon IN-713 superalloy for integral turbine wheels, weldable blades and high-fatigue hot-section castings, supplied as master alloy ingot or precision investment castings.
Inconel 713LC (IN-713LC) is the low-carbon member of the IN-713 cast superalloy family. It keeps the same nickel-chromium-aluminium-molybdenum-niobium base and the same gamma-prime Ni3(Al,Ti) strengthening that gives the family its high-temperature strength, but holds carbon to 0.05% maximum. That single change reduces grain-boundary carbide embrittlement and lifts room-temperature ductility, low-cycle fatigue life and weldability — the three properties that matter most in a rotating, thermally cycled cast component.
As a cast-only alloy, 713LC is produced exclusively by vacuum induction melting and vacuum investment casting. It is the standard choice for integral turbine and turbocharger wheels, where the whole rotor is cast as one piece, and for blades and vanes that must tolerate weld repair or aggressive start-stop thermal cycling. Hangbo Alloy supplies it as master alloy ingot and as near-net-shape investment castings to AMS 5377.
The governing specification is AMS 5377, whose title names the chemistry directly: nickel alloy, corrosion- and heat-resistant, investment castings, 73Ni-12Cr-4.5Mo-2.0Cb(Nb)-0.70Ti-0.05C-6.0Al-0.010B-0.10Zr, vacuum cast, as-cast. ASTM B637 applies where master alloy or remelt stock is specified, and OEM specifications such as B50T1239, MSRR 7048 and EMS 55079 are also common in aerospace orders. The standard-carbon parent grade is our Inconel 713C page.
The alloy is normally delivered in the as-cast condition, which already carries full gamma-prime strengthening. Where maximum creep life or ductility is required, a homogenisation solution treatment followed by double ageing is applied, always with air or furnace cooling — water quenching is avoided because thick cast sections crack.
| Element | Ni | Cr | Mo | Al | Nb (Cb) | Ti | C | Zr | B | Co | Fe | Si | Mn |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Nominal (wt%) | Bal | 12.0 | 4.5 | 6.0 | 2.0 | 0.70 | ≤0.05 | 0.10 | 0.010 | ≤1.0 | ≤0.50 | ≤0.50 | ≤0.25 |
Nominal composition to AMS 5377. Carbon is held to 0.05% maximum for ductility and weldability; individual heats are certified on the mill test certificate.
| Property | Value (as-cast) |
|---|---|
| Tensile strength, room temperature | ≈820–850 MPa |
| Yield strength (0.2%), room temperature | ≈700 MPa |
| Elongation, room temperature | 8–15% |
| Stress-rupture life, 980 °C / 152 MPa | ≥ 30 h |
| Service temperature limit | ≈950 °C |
| Density | 7.91 g/cm³ |
| Melting range | 1260–1364 °C |
| Magnetic | Non-magnetic (austenitic) |
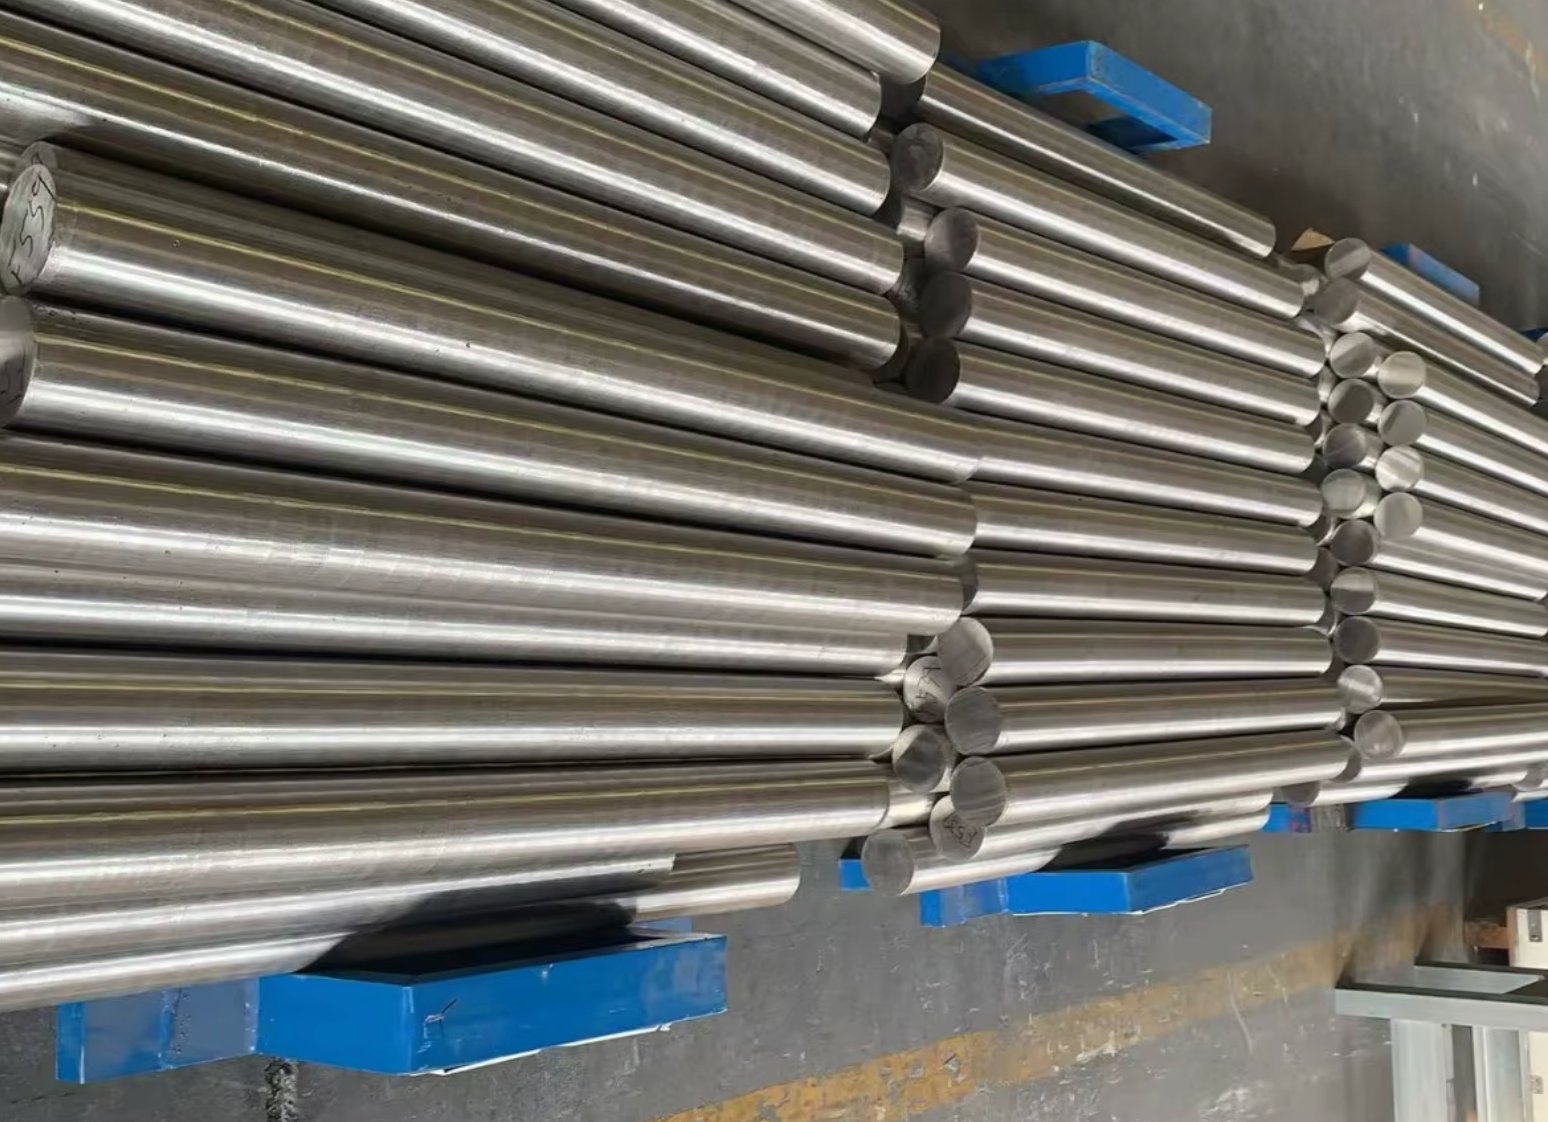
Master alloy ingot. Vacuum induction melted remelt sticks, typically 75 mm and 90 mm diameter, with chemistry certified to AMS 5377 and the customer's own specification, for foundries running investment-casting or directional-solidification lines.
Precision investment castings. Near-net-shape castings produced from your CAD or pattern, in equiaxed grain or, where specified, directionally solidified (DS) structure. Typical parts are integral turbine and turbocharger wheels, blades, nozzle guide vanes, shrouds and thin-walled hot-section components with internal cooling passages.
Post-processing. Hot isostatic pressing (HIP) to close casting porosity and lift high-cycle fatigue life, radiographic and fluorescent penetrant inspection on rotating parts, and controlled-window machining of castings with carbide and PCD tooling.
Every shipment carries an EN 10204 3.1 mill test certificate stating heat number, full chemical analysis including carbon, boron and zirconium, the heat-treatment condition and tensile plus stress-rupture results. EN 10204 3.2 independent verification and third-party inspection through BV, SGS, TUV or DNV are available. Our quality system is certified to ISO 9001:2015 and GJB 9001C, and master alloy can be held against your release schedule so casting runs never wait on material.
Send us your casting drawing or master alloy specification — grade, weight, quantity and any DS or HIP requirement — and our team responds within 10 minutes during business hours.